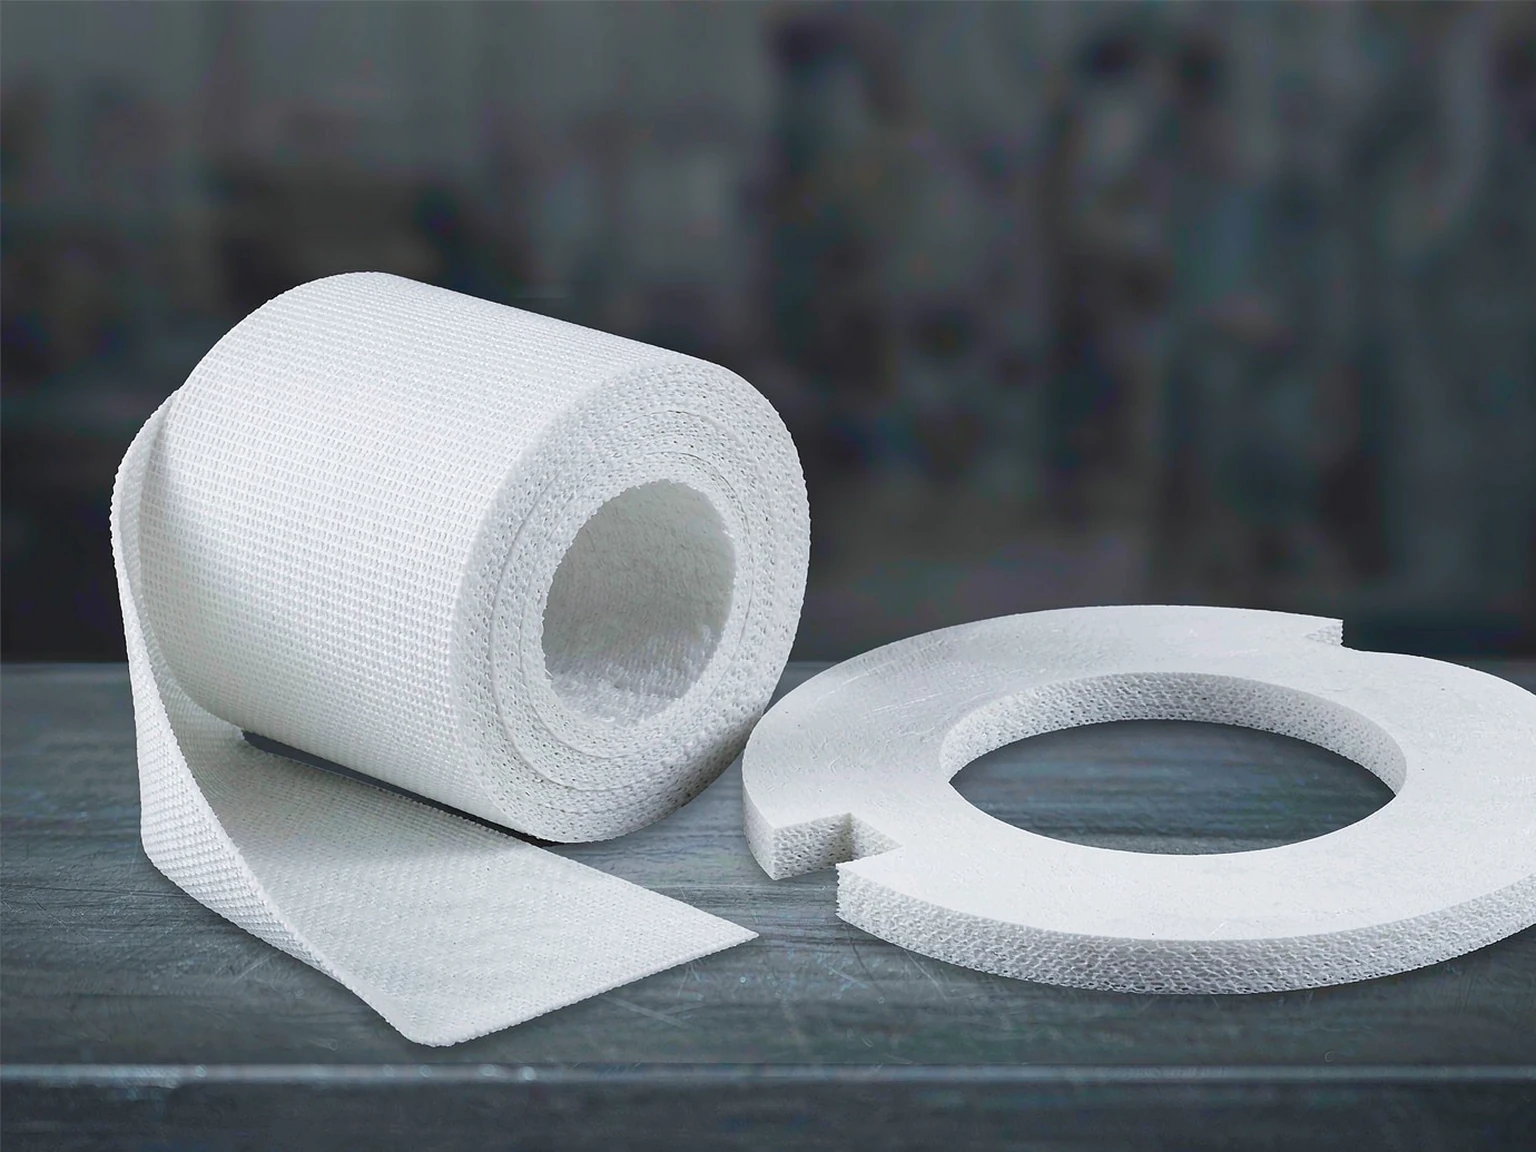
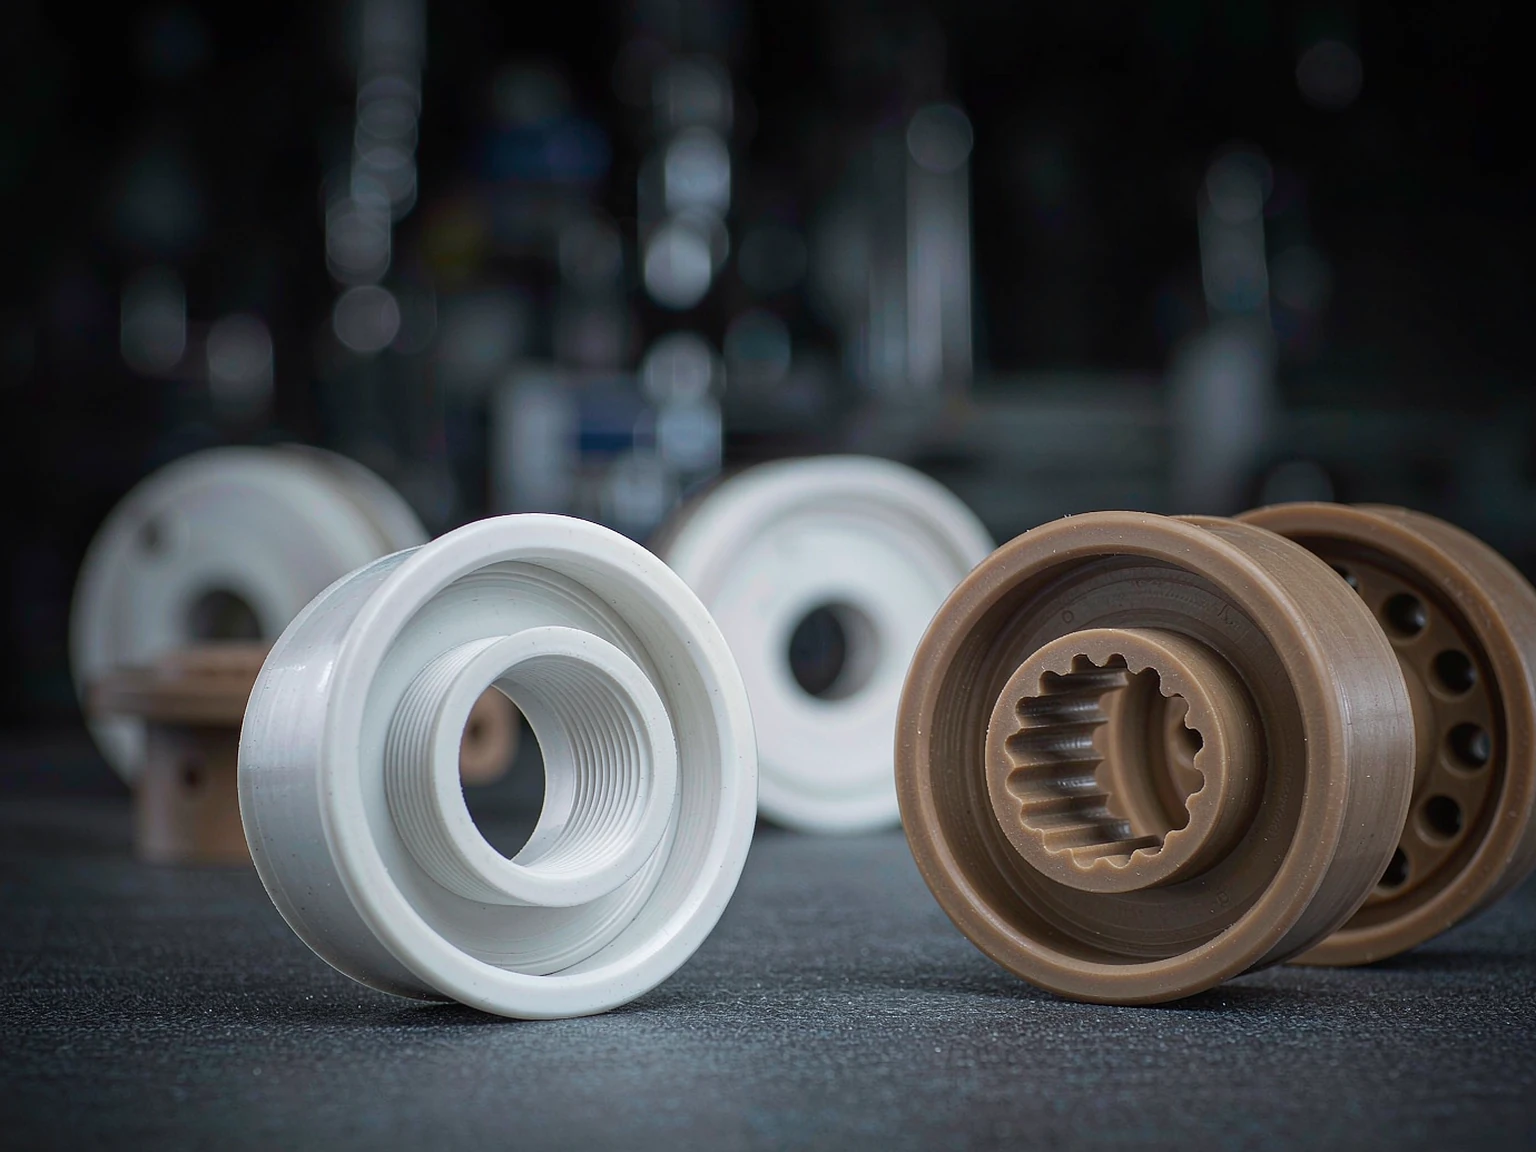
Short answer: define PTFE machining surface finish by function, not by copying metal Ra callouts: sealing faces need smooth uniform finish (Ra ~0.8–1.6 μm achievable), sliding counterfaces need controlled texture and lay, and structural parts need only burr-free cleanliness. State the function; the toolpath follows.
What PTFE can achieve — and what it does differently
PTFE machines to good finishes but its low modulus means the cut deforms the surface layer; tool sharpness, speeds and coolant discipline matter more than spindle power. Feathered edges and smearing are the typical defects — both process-controlled.
Specifying without over-specifying
- Sealing faces: Ra 0.8–1.6 μm, no tool marks across the seal line.
- Sliding surfaces: finish AND direction of marks matter (wrong lay increases wear).
- Everything else: “clean, burr-free” — metal-grade Ra values just add cost.
Chunhuan machines PTFE with process-controlled finishing since 1985 — stock and machining program. Mark functional surfaces on the drawing; expect the finish strategy per surface in the quote.
Frequently Asked Questions
What surface finish can machined PTFE achieve?
About Ra 0.8-1.6 µm on sealing faces with controlled toolpaths; function-appropriate finishes elsewhere without metal-grade premiums.
Why not copy metal Ra callouts to PTFE drawings?
PTFE’s low modulus deforms under the cut; metal-grade finish specs add cost without function. Define by part function instead.
Does surface lay matter on PTFE sliding parts?
Yes — mark direction relative to sliding; wrong lay raises wear on some filled grades.

 English
 Russian
 French
 Spanish
