Short answer: for pharmaceutical processing, verify PTFE components on four fronts: compliance (FDA 21 CFR 177.1550, USP Class VI where contact applies, RoHS/REACH), purity (extractables, no pigments/fillers unless qualified), traceability (resin lot to shipment), and surface/cleanability (finish, dead-space-free geometry). The verification is documentary — build it into the PO.
The verification list
- Compliance certificates naming the regulation, not “food grade” adjectives.
- Extractables data with method and limits, per lot for product-contact parts.
- https://ptfesuppliers.com/product-category/rade purity: virgin resin only for contact parts; filled grades need explicit qualification.
- Finish and geometry: smooth bore, radiused corners, CIP-compatible design.
- Lot traceability end to end — the audit question is “prove this part’s history”, and the answer must be a paper trail.
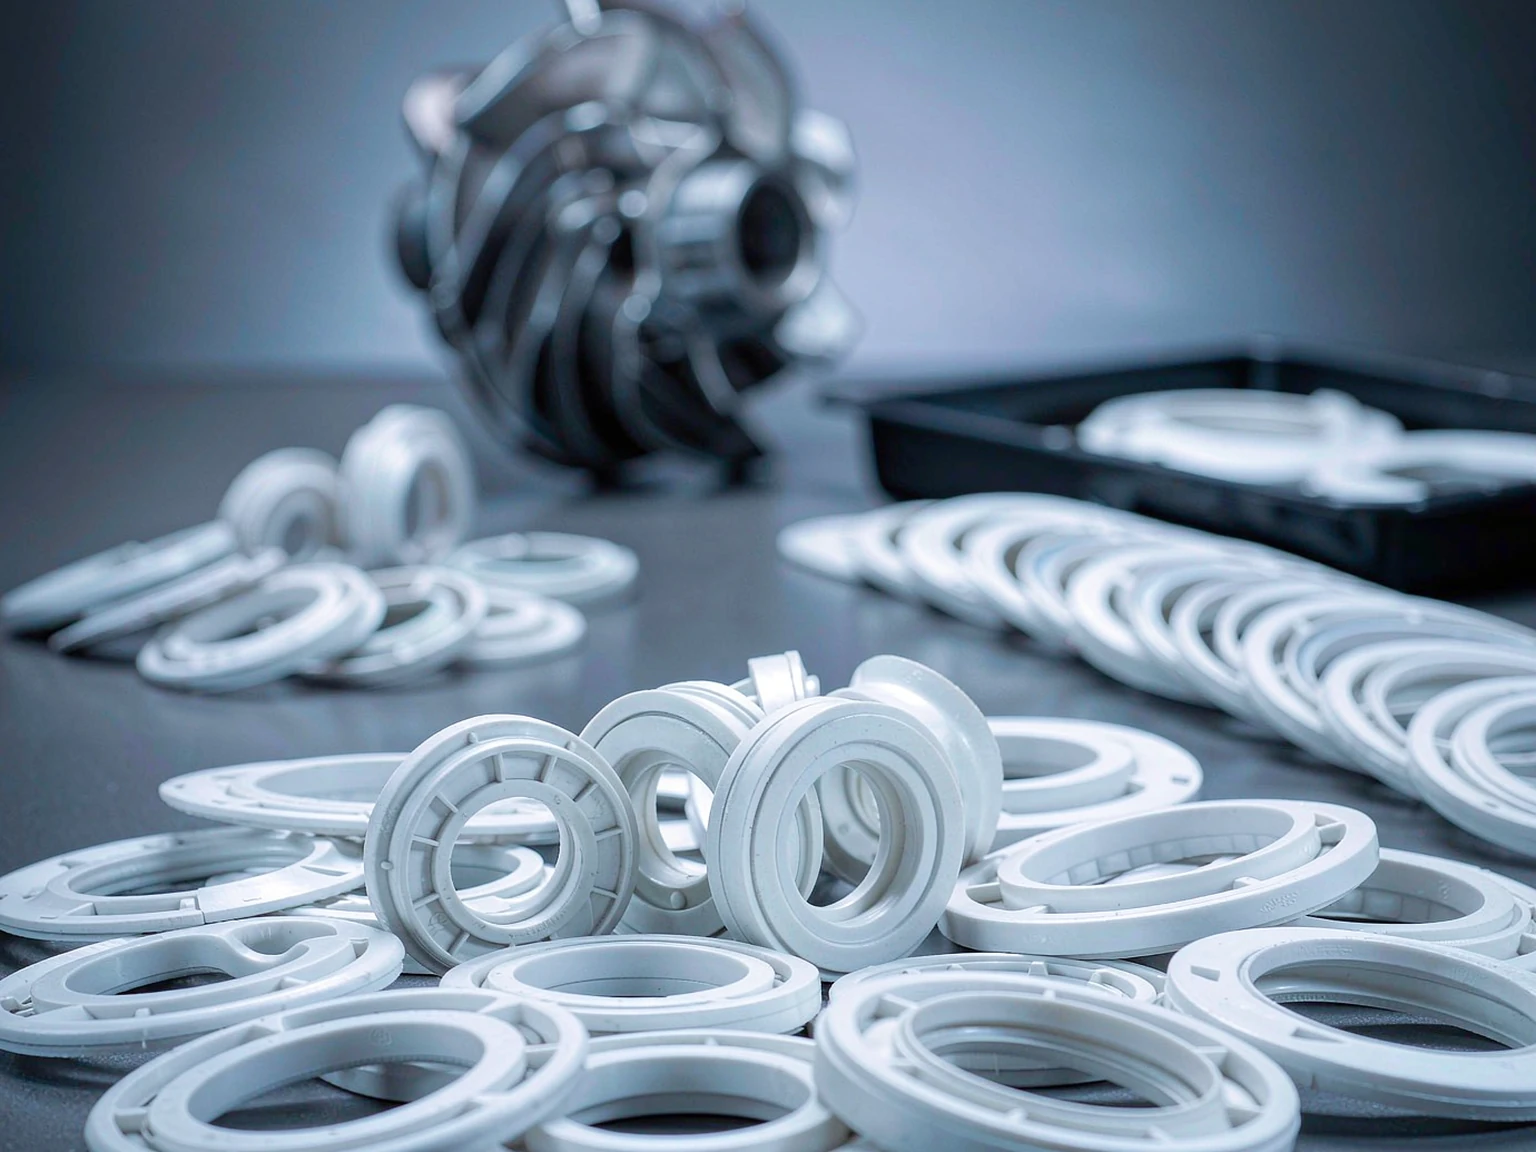
Chunhuan supplies FDA-documented PTFE components since 1985 — stock shapes and machined parts with lot certificates. Send the contact class (product contact vs utility); the documentation set follows from it.
Frequently Asked Questions
What certifications do pharma PTFE parts need?
FDA 21 CFR 177.1550 compliance, USP Class VI where contact applies, RoHS/REACH, with lot traceability end to end.
Can filled PTFE be used in pharma?
Only with explicit qualification — product-contact parts default to virgin resin for extractables and cleanability.
What surface requirements matter?
Smooth, crevice-free geometry compatible with CIP/SIP; cut-end quality and finish should be specified, not assumed.

 English
 Russian
 French
 Spanish
