Choose PTFE rods when your application needs the lowest friction coefficient (0.04–0.10), continuous service up to 260°C, near-universal chemical resistance, and food or medical compliance — and when mechanical load is light to moderate. Choose PEEK rods instead when you need high stiffness, load-bearing strength above 100 MPa, or wear resistance under pressure at elevated temperatures. If your part slides against a soft metal, runs in strong acid, or must pass FDA food contact, PTFE is the answer.
By the end of this article, you will be able to run a five-step selection check on any rod application and state, in one sentence, whether PTFE or PEEK is the correct material.
Table of Contents
Why the Two Materials Behave Differently

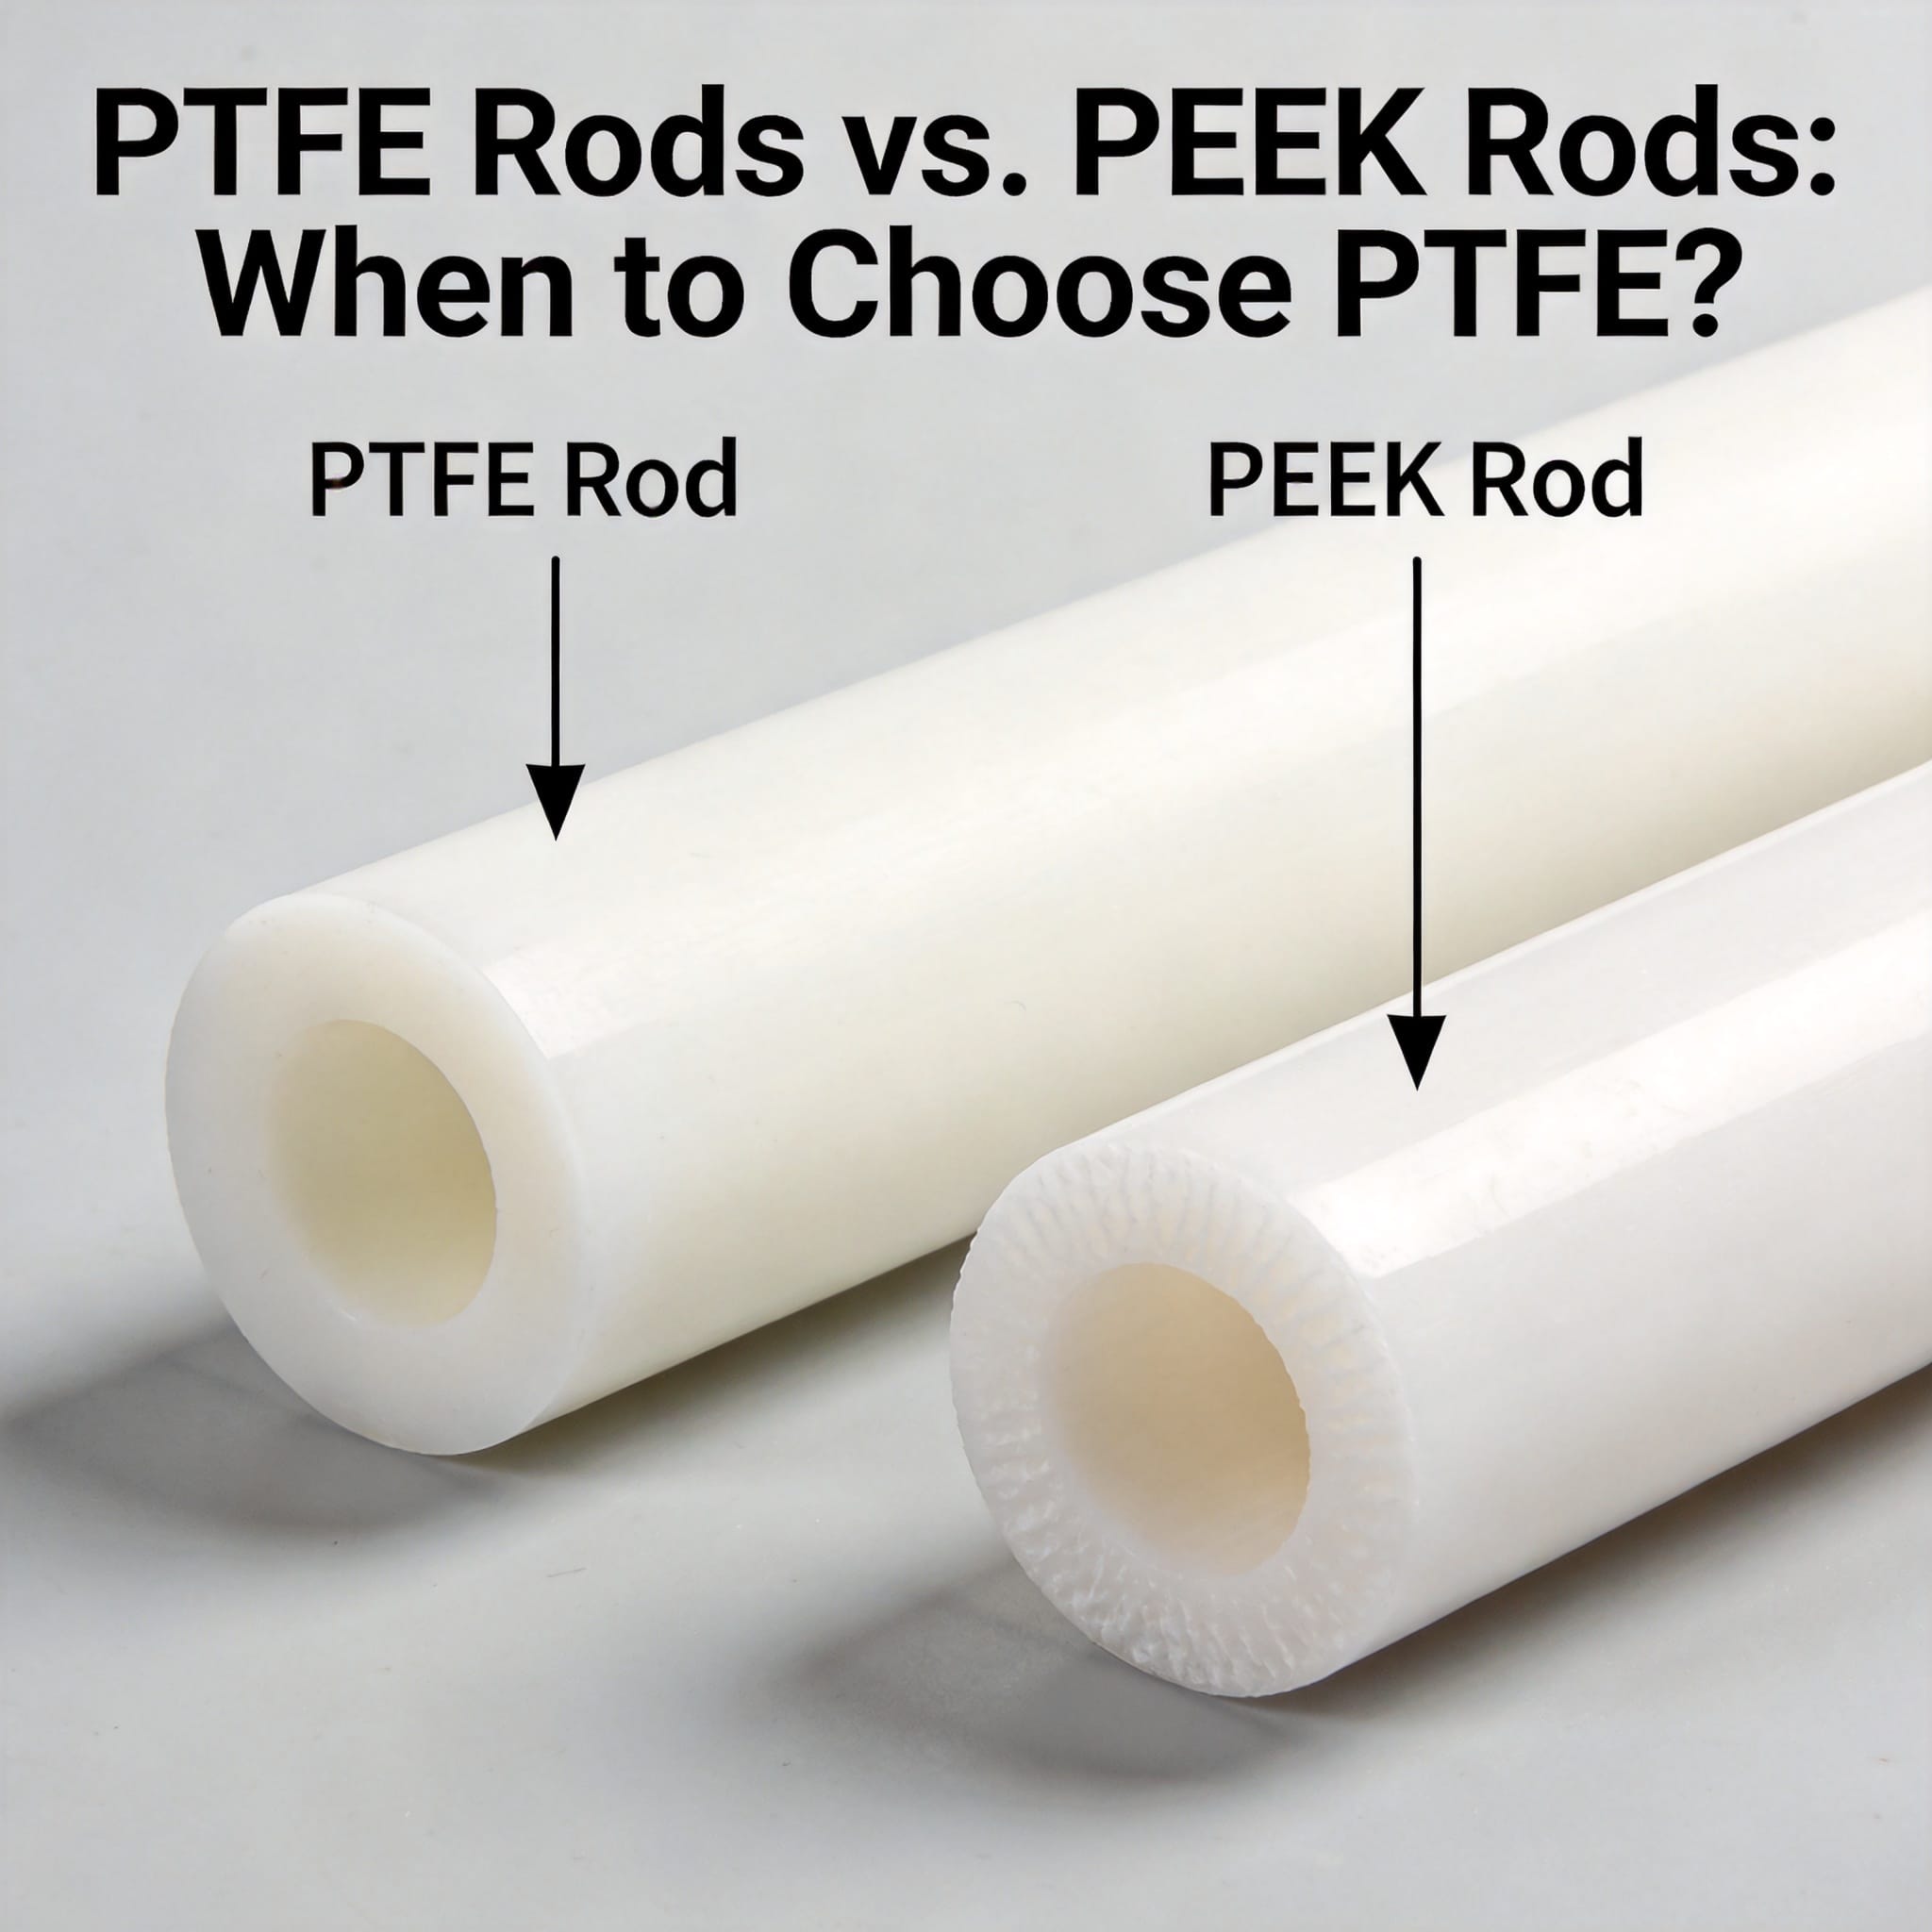
PTFE (polytetrafluoroethylene) is a linear fluoropolymer built from carbon–fluorine bonds. Those bonds are extremely strong and the fluorine shell shields the carbon backbone, which is why PTFE resists almost every industrial chemical and has one of the lowest friction coefficients of any solid — 0.04 to 0.10 against steel. The trade-off is mechanical: virgin PTFE has a tensile strength of roughly 20–35 MPa and creeps under sustained load.
PEEK (polyetheretherketone) is a semi-crystalline aromatic thermoplastic with a rigid backbone. It reaches 90–100 MPa tensile strength, a flexural modulus near 3.6–4.0 GPa, and continuous service around 250°C with a melting point of 343°C. It wears far better under load, but its friction coefficient is roughly 0.30–0.40 — three to five times higher than PTFE.
The practical consequence: PTFE wins on friction and chemistry, PEEK wins on strength and wear. Most selection errors come from ignoring which of these two axes your application actually stresses. For background on how these values are measured, see the NIST materials data portal and the ASTM standard library for D638 (tensile) and D790 (flexural) test methods.
How to Choose: A 5-Step Decision Process
Work through these steps in order. Stop at the first step that gives a definitive answer.
- Check the chemical environment. If the part contacts strong acids, bases, solvents, or oxidizing agents, select PTFE. PEEK is attacked by concentrated sulfuric acid, halogens, and some ketones. This single check resolves most chemical-processing applications.
- Check the continuous temperature. Below 250°C, either material can work. From 250–260°C, PTFE remains stable but PEEK approaches its glass transition region and loses stiffness. Above 260°C, PTFE is the safer choice for continuous duty.
- Check the load. Calculate the compressive stress on the part. If it exceeds roughly 7 MPa continuously, virgin PTFE will cold-flow and deform. Either switch to PEEK or specify a filled PTFE grade (glass, carbon, or bronze filled) that raises creep resistance.
- Check the sliding speed and counterface. For high-speed, low-load sliding against soft metals like aluminum or brass, choose PTFE — it will not gall or scratch the mating surface. For slow, high-load bearing surfaces, choose PEEK.
- Check the compliance requirement. If the part needs FDA food-contact status, USP Class VI biocompatibility, or low extractables, confirm the specific grade’s certification. Both base polymers can qualify, but only certified grades may be used.
Example: A pump seal lip running in 20% hydrochloric acid at 80°C against a stainless shaft, with 2 MPa contact pressure. Step 1 gives the answer immediately — PTFE. PEEK would degrade in the acid over time.
Counter-example: A thrust washer in a gearbox carrying 25 MPa at 120°C. Step 3 eliminates virgin PTFE due to creep; PEEK is correct.
PTFE vs. PEEK: Side-by-Side Data
| Propiedad | PTFE (virgin) | PEEK |
|---|---|---|
| Tensile strength | 20–35 MPa | 90–100 MPa |
| Flexural modulus | 0.5–0.8 GPa | 3.6–4.0 GPa |
| Coefficient of friction vs. steel | 0.04–0.10 | 0.30–0.40 |
| Continuous service temperature | 260°C | 250°C |
| Melting point | 327°C | 343°C |
| Chemical resistance | Near-universal | Good, but attacked by concentrated acids and halogens |
| Water absorption (24 h) | <0.01% | ~0.15–0.5% |
| Creep resistance | Poor (virgin) | Excellent |
| Machinability | Soft, gummy, requires sharp tooling | Rigid, machines like hard plastic |
| Relative material cost | Low | High (typically 5–10× PTFE) |
Notice the pattern: PTFE dominates the friction, chemistry, and moisture columns; PEEK dominates the strength, stiffness, and creep columns. Cost follows the same split. When two materials are this cleanly separated, the decision usually comes down to a single dominant requirement rather than a weighted average. For a closer look at how these properties translate into finished parts, see these custom PTFE rods for corrosion-resistant sealing and insulating applications.
Common Mistakes and How to Fix Them
Mistake 1: Using virgin PTFE under sustained load
Symptom: The rod flattens, elongates, or loses dimensional tolerance after weeks in service, even though nothing broke. Fix: Either reduce continuous stress below ~7 MPa, switch to a filled PTFE grade, or move to PEEK. Creep is time-dependent, so a part that passes a short bench test can still fail after 500 hours. A glass fiber reinforced PTFE rod is one option that raises creep resistance while keeping most of PTFE’s chemical and friction advantages.
Mistake 2: Choosing PEEK for chemical contact without checking the medium
Symptom: The PEEK part swells, crazes, or embrittles after exposure to concentrated sulfuric acid or a halogenated solvent. Fix: Verify compatibility against a chemical resistance chart before specifying. When in doubt with aggressive media, PTFE is the conservative choice.
Mistake 3: Ignoring the counterface material
Symptom: An aluminum or brass shaft wears rapidly when paired with a PEEK bushing, or the polymer itself galls. Fix: Pair PTFE with soft counterfaces. If you must use PEEK, harden and polish the mating surface, or add a lubricant.
Mistake 4: Assuming higher cost means better performance
Symptom: A PEEK part is specified for a low-load, high-speed sliding application and fails early from friction heating. Fix: Match the material to the dominant failure mode. In low-load sliding, PTFE’s low friction outperforms PEEK regardless of price.
Preguntas frecuentes
Can I use PTFE rods in a bearing application?
Yes, if the load is light and the speed is high. PTFE’s low friction makes it ideal for non-lubricated bearings, but keep continuous compressive stress below about 7 MPa or use a filled grade.
Is PEEK always stronger than PTFE?
In tension, flexure, and creep resistance, yes — by roughly three to five times. But strength is not the only criterion. In chemical resistance and friction, PTFE is clearly superior.
Which material is easier to machine?
PEEK. It is rigid and produces clean chips. PTFE is soft and gummy, so it requires sharp tooling, slower feed rates, and careful chip evacuation to avoid dimensional drift from thermal expansion.
What temperature limit should I use for PTFE?
Plan for a continuous service ceiling of 260°C. Brief excursions higher are tolerable, but sustained operation above that accelerates degradation and dimensional change.
Do both materials meet food-contact requirements?
Base polymers can, but compliance is grade-specific. Confirm that the exact grade you order carries the relevant FDA or EU 10/2011 declaration before use. For high-purity needs, a virgin PTFE rod is a good starting point.
When is the decision genuinely close?
When the application is below 200°C, at moderate load (5–10 MPa), and in a benign chemical environment. In that narrow band, choose PTFE if friction or cost dominates, and PEEK if dimensional stability dominates. If you need a rod tailored to a specific grade or dimension, custom 100% virgin PTFE rod options are worth reviewing.

 English
 Russian
 French
 Spanish
