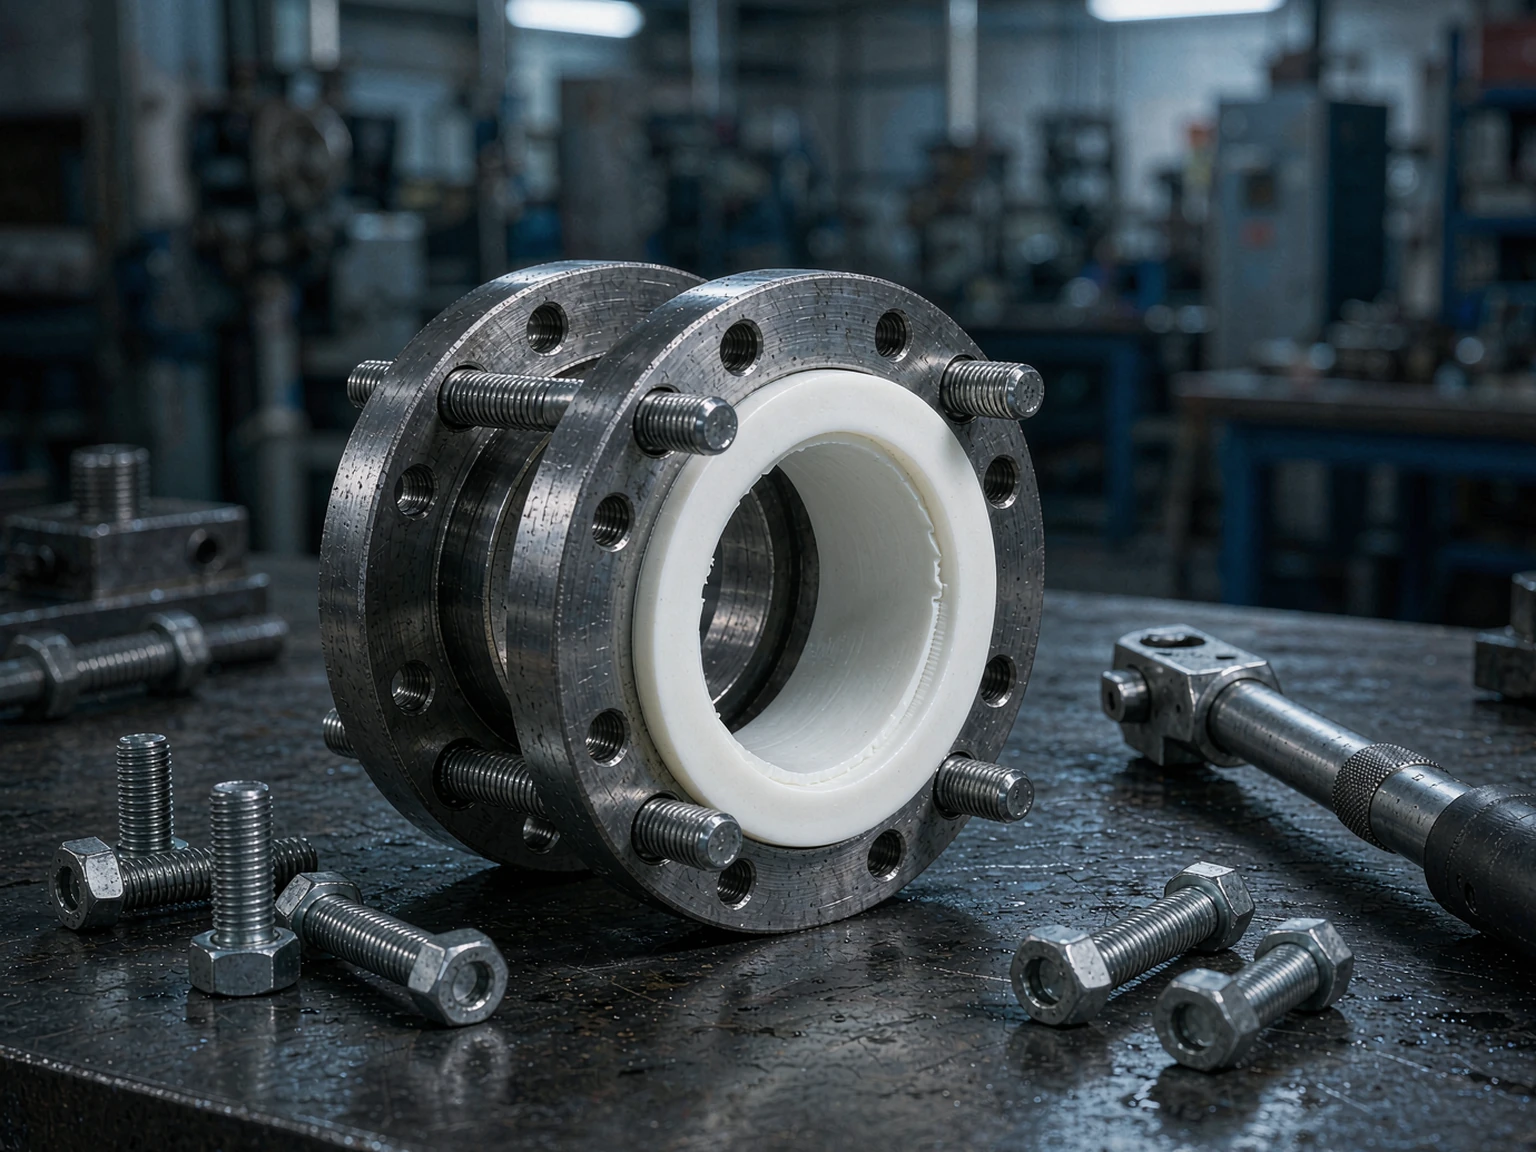
Short answer: PTFE gasket creep (cold flow) is sustained-stress deformation that thins the gasket and relaxes bolt load — the number-one field failure of PTFE seals. Designers manage it with three levers: grade (fillers cut creep 2–5x), thickness (thinner creeps less), and stress design (controlled bolt practice).
Why cold flow happens
Under sustained bolt stress PTFE deforms plastically — slowly at room temperature, faster hot. The gasket thins, bolt load drops, and the joint weeps at the next thermal cycle. Chemicals are rarely involved; time, temperature and stress are.
The three levers, quantified
- https://ptfesuppliers.com/product-category/rade: 15–25% glass or bronze filler improves creep resistance 2–5x; expanded PTFE’s fibrils also resist flow better than virgin.
- Thickness: creep scales with thickness under the same stress — the thinnest gasket that seals is the best one.
- Stress design: adequate but not excessive seating stress, torque tables, and re-torque after the first thermal cycle to reset the relaxation.
Chunhuan publishes deformation-under-load data per grade across its gasket program since 1985. Send temperature, bolt stress and cycling; the answer should include a creep-relevant grade and a re-torque recommendation.
Frequently Asked Questions
Why do PTFE gaskets thin over time?
Cold flow: sustained bolt stress deforms PTFE plastically, faster at temperature. Manage with filled grades, thinner sections and controlled stress.
How much do fillers reduce creep?
Typically 2-5x depending on filler type and content — the main reason filled gaskets hold hot flanges.
Is re-torque really necessary?
Yes — after the first thermal cycle, relaxation is at its peak. A documented re-torque resets the joint cheaply.

 English
 Russian
 French
 Spanish
